Press Compatibility and Die Handover
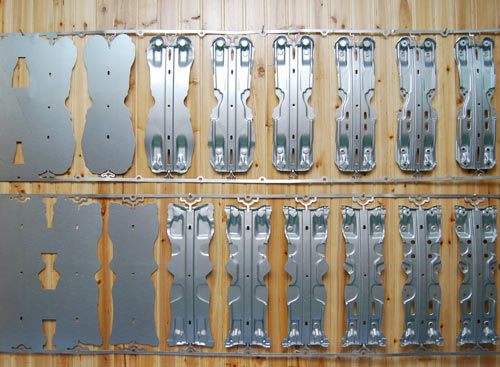
Standalone Stamping Die Examples
Standalone stamping dies manufactured around receiving-press compatibility, trial requirements and documented handover conditions.
- Process
- Standalone stamping die with an agreed pre-shipment trial
- Materials
- Trial sheet grade and thickness per specification
- Quantity
- Die quantity and trial sample count per project
- Inspection
- Press interface review and trial-piece approval
Product Overview
GPT Precision manufactures standalone stamping dies according to approved project requirements.
A die must not only produce acceptable parts during a trial; it must also be compatible with the receiving production equipment.
This requires reviewing the intended press and operating arrangement before finalizing the tooling design.
Key Features
- The die mounting pattern should be checked against the receiving press specifications.
- Die closed height and the press's available shut-height range must be compared using corresponding reference surfaces and the intended bolster or spacer arrangement.
- Other relevant requirements may include feed direction, available stroke, material entry, part removal and scrap clearance.
Manufacturing Considerations
- Trial requirements are agreed for each project.
- The trial basis should identify the applicable drawing revision, sheet material, thickness, press arrangement, feed conditions and required sample quantity.
- Use the receiving press specification to check die compatibility. Record and review differences between the agreed pre-shipment trial setup and the receiving press setup that could affect transfer.
Quality Control & Inspection
- Trial parts are inspected against the approved drawing and agreed criteria.
- Requirements may include hole dimensions, formed geometry, burr limits and other critical features.
- Once the agreed pre-shipment trial is complete and the trial samples are approved, the die is packed. The customer arranges collection and transport.
- Handover documents, setup information and any additional acceptance conditions should be confirmed before transfer.
Specifications to Confirm
| Receiving press | Provide the mounting pattern and usable press dimensions. |
|---|---|
| Die closed height | Identify the reference surfaces and intended bolster or spacer arrangement. |
| Feed and clearance | Confirm stock entry, feed direction, part removal and scrap clearance. |
| Trial setup | Agree trial equipment, drawing revision, sheet grade, thickness and feed conditions. |
| Trial samples | Confirm sample quantity, critical dimensions and applicable edge or burr criteria. |
| Handover | Agree the trial records and transfer documents. After sample approval, the die is packed for customer-arranged collection and transport. |
Assembly Considerations
Mounting and Shut Height
Compare the die mounting arrangement with the receiving press and check closed height against the available shut-height range.
Stock, Parts and Scrap
Review feed alignment and the paths for part removal and scrap clearance in the intended setup.
Related Products

Request a Stamping Die Quote
Send your part drawing, sheet-metal specification, expected production volume and receiving press information. Include existing die drawings or machine-interface requirements where available.